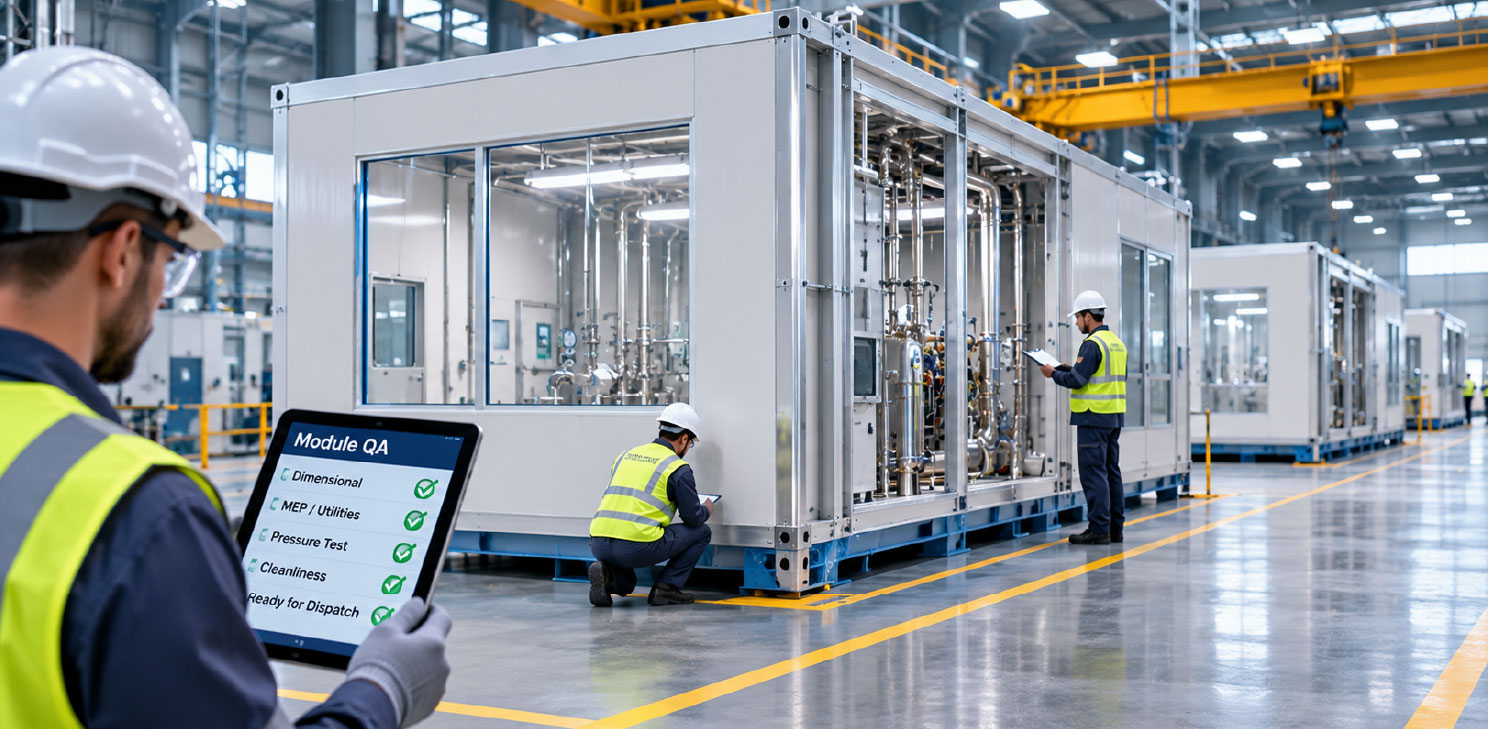
Prefabricated modules move much of the work into the factory, where framing, services and insulation disappear behind linings as production advances. Effective quality control prefabricated modules programs therefore inspect work while it is still accessible, test equipment before shipment and carry the evidence through installation and commissioning.
Set Acceptance Criteria Before Production
Quality assurance establishes procedures and responsibilities. Quality control verifies the work through inspections, testing and documented results. An inspection and test plan connects the two by stating what is checked, when, by what method, against which acceptance limit and who signs off. Vague criteria should give way to measurable tolerances tied to approved drawings and codes.
Define hold points, where work cannot proceed without release, and witness points, where a designated party may observe. Agree how results will be categorized, such as pass, conditional pass or hold, before testing begins, since debating severity under schedule pressure produces poor decisions. Because modules cross jurisdictional lines, also confirm which codes apply at the destination.
Inspect Station by Station for Quality Control Prefabricated Modules
Each production station offers a natural checkpoint. Inspectors verify that incoming materials match specifications and that certificates are matched to the actual batch. They then confirm that prior-station work passed before checking the work completed at the current station. Measurements and photographs recorded against the specific module build a traceable history.
Concealed work deserves hold points. Structural joints, service supports, insulation continuity and fire-stopping should be examined before enclosure. Dimensional checks belong at each meaningful stage, not only at the end of the line, because a marginally out-of-spec module can cause misaligned connections and failed inspections on site.
When a check fails, record what failed, where and on which unit. Assign corrective action and re-inspect against the original criteria before closing the item, because verbal confirmation is not enough. Repetition spreads errors, so inspect other units built with the same setup.
Witness Factory Acceptance Testing
Factory acceptance testing (FAT) proves equipment works at the manufacturer’s facility, where calibrated instruments, spare parts and experienced technicians are on hand. Field repairs often cost several times more than equivalent factory repairs, so catching problems before shipment pays for itself.
Prepare first. Require complete assembly, finished internal testing, calibration certificates and a signed readiness checklist before anyone travels. Build a witness team that includes project engineers, quality personnel, operations representatives and, for safety systems, safety specialists.
Then scope the test to the module type. For modular data centers, mark the test boundary on the approved single-line and piping diagrams, place simulated heat where it will actually travel and record every temporary or simulated interface. For prefabricated substations, FAT begins with a kickoff meeting that defines scope, responsibilities and timelines. Strict safety controls apply, and functional tests then cover switchgear, fire detection, HVAC and interlocks. Test fail-safe behavior, including power loss, rather than reviewing logic on paper.
Release, Transport and Commissioning for Quality Control Prefabricated Modules
Treat factory release as a documented decision covering dimensions, identification, completed inspections, test results, protective measures and open defects. Separate shipment release from final facility acceptance, and state clearly what remains for site testing. Conditional release needs an authorized decision, explicit restrictions and a named owner for closure.
Transport can invalidate earlier acceptance. On receipt, check for distorted frames, torn weather protection and signs of water entry, and repeat any earlier checks that handling may have affected. Before lifting, confirm foundation positions and anchor locations against the coordinated design. Give intermodule joints separate attention for structural continuity, weather resistance, fire separation and services.
Completed-building tests then verify integrated performance. These include water-tightness, airtightness, electrical, plumbing, ventilation balancing and controls commissioning. Factory results cannot prove that site joints and connections perform correctly.
Make Records a Lasting Asset
Keep approved procedures, as-tested configurations, raw test data, calibration records and an open-item register with named owners. These records become the maintenance baseline for decades. Strong quality control prefabricated modules practice means every handover, from station to shipment to site, is verified, recorded and traceable.
To find out more about the latest industry updates and innovations in prefabrication for mega facility construction, meet with solution providers and hear talks from expert speakers, attend the Prefabrication for Mega Facilities Summit USA, taking place November 17-18, 2026, in Houston, Texas, USA.
For more information, click here or email us at info@innovatrix.eu for the event agenda. Visit our LinkedIn to stay up to date on our latest speaker announcements and event news.